

แม่พิมพ์รองเท้า 3D พิมพ์จากเหล็กกล้าสแตนเลส, อลูมิเนียม และเหล็ก MS1 Maraging | ศึกษากรณีแม่พิมพ์รองเท้า SLM
แม่พิมพ์รองเท้า 3D พิมพ์ด้วยโลหะจากเหล็กกล้าสแตนเลส 316L, อลูมิเนียม AlSi10Mg และเหล็ก MS1 (1.2709) แบบ maraging แม่พิมพ์รองเท้า SLM ที่มีช่อระบายความร้อน conformal, แกน lattice แบบบูรณาการและเนื้อผิวแบบ pin-array ลดเวลาในรอบการผลิตลง 50% ลดเวลาการจัดส่งลง 80% และเสรีภาพในการออกแบบ 100% เทียบกับแม่พิมพ์อลูมิเนียม CNC
Case Study: 3D-Printed Shoe Molds —
Stainless Steel, Aluminum & MS1
SLM Metal 3D Printing | Conformal Cooling | Multi-Material Footwear Tooling
Footwear Tooling Case Study
1. Background
A global athletic footwear brand was launching a new line of performance running shoes with a fully re-engineered midsole lattice and a new outsole tread pattern. The legacy CNC-machined aluminum molds could not deliver the required internal lattice geometry, the integrated pin arrays, or the conformal cooling channels needed for a 50% faster cycle time on the new EVA-foam direct-injection line. The brand needed four distinct mold types — a midsole direct-foaming mold, a dual-cavity outsole mold with pin arrays, a perforated tread mold, and a shoe last (upper) mold — each optimized for a different material system and cycle profile. SLM metal 3D printing, in three different alloys, delivered all four in a single supply chain.
2. The Challenge
Design requirements included:
· Midsole direct-foaming mold in AlSi10Mg aluminum — 50% cycle-time reduction via internal conformal cooling channels
· Outsole mold in MS1 (1.2709) maraging steel — HRC 50–55 after aging, mirror-polished wear surface for EVA / TPU injection
· Perforated outsole mold in 316L stainless steel — 1000+ precision perforations, corrosion-resistant for foaming-agent service
· Shoe last (upper) mold in 316L stainless steel — patient-specific geometry per size, with mesh perforation pattern for upper-forming
· All four mold types delivered within 4 weeks, ready for first-article trials
· Multi-alloy platform: each mold matched to its specific duty (aluminum for fast cycle, MS1 for high-pressure wear, 316L for corrosion / hygiene)
· 100% design freedom — lattice cores, conformal cooling, pin arrays printed as monolithic features with no assembly
3. The Solution
The four mold types were designed as monolithic parts, each matched to its specific duty cycle, and manufactured by Selective Laser Melting (SLM) in three different alloys. The midsole direct-foaming mold was printed in AlSi10Mg aluminum with topology-optimized internal conformal cooling channels that follow the cavity contour — cooling time dropped from 120 s to 60 s, the cycle-time reduction the brand was looking for. The dual-cavity outsole mold with pin arrays was printed in MS1 (1.2709) maraging steel, then aged to HRC 50–55 and mirror-polished on the wear surface for direct EVA / TPU injection. The perforated outsole mold was printed in 316L stainless steel with 1000+ precision perforations, the corrosion resistance needed for foaming-agent service. The shoe last mold was printed in 316L stainless steel with patient-specific geometry per shoe size, with a mesh perforation pattern for the upper-forming line.
Each mold was delivered with its own post-processing recipe: the aluminum midsole mold was stress-relieved and bead-blasted; the MS1 outsole mold was aged to HRC 50–55 and mirror-polished on the wear face; the 316L outsole mold was passivated per ASTM A967 and electropolished on the perforations; the 316L last mold was bead-blasted to a uniform satin finish. All four were delivered in 2-4 weeks, vs. the 12-16 week lead time of conventional CNC-machined aluminum molds.
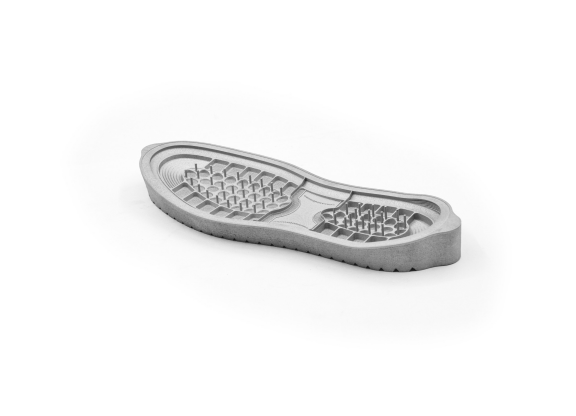
Figure 1: SLM-printed AlSi10Mg midsole direct-foaming mold — internal conformal cooling channels (50% cycle-time reduction)
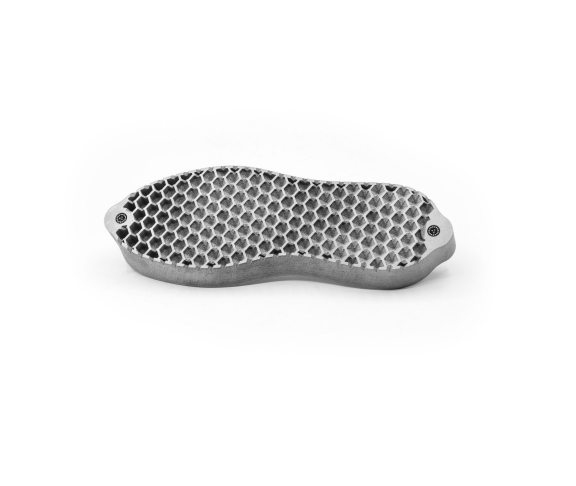
Figure 2: Same AlSi10Mg midsole mold — cavity side showing the as-built lattice and pin-array textures
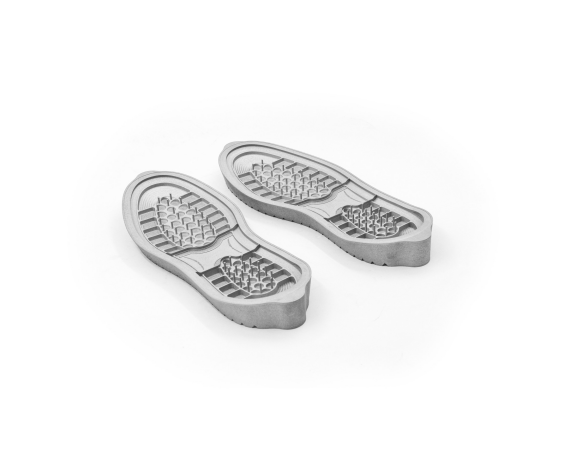
Figure 3: SLM-printed MS1 (1.2709) maraging steel outsole mold pair (left/right) — pin-array cavity, HRC 50–55 after aging, mirror-polished wear surface
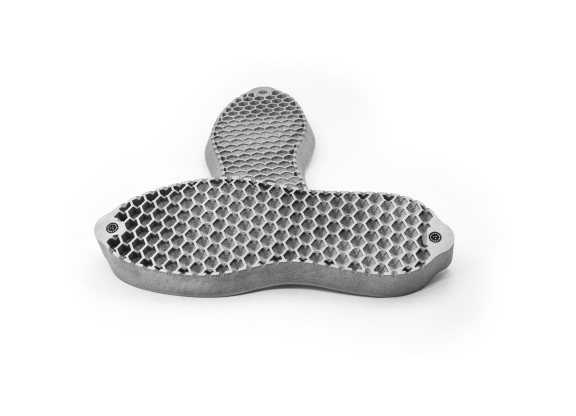
Figure 4: Same MS1 outsole mold pair — angled view showing the ejector-pin layout and the monolithic maraging steel construction
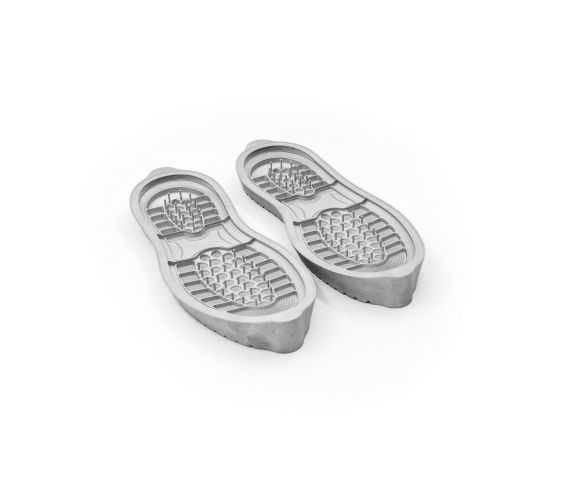
Figure 5: SLM-printed MS1 outsole mold — close-up of the pin-array cavity and the lattice / texture transitions
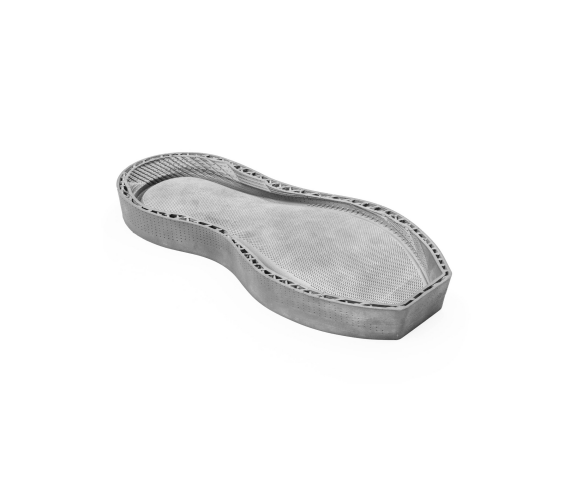
Figure 6: SLM-printed MS1 outsole mold — inverted view showing the flow channels and the cooling-line routing
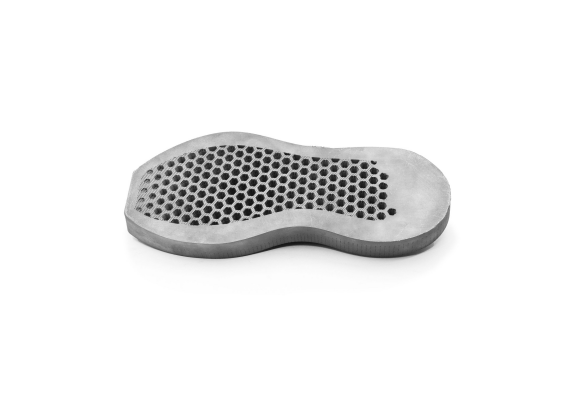
Figure 7: SLM-printed 316L stainless steel perforated outsole mold — 1000+ precision perforations, corrosion-resistant for foaming-agent service
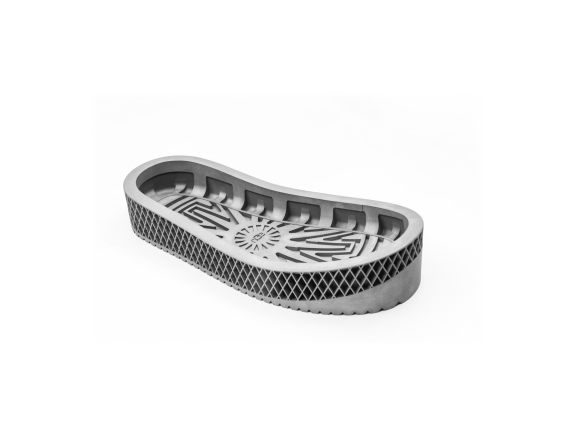
Figure 8: SLM-printed 316L midsole mold with diamond cross-hatch traction pattern (UGG-style) and tread perimeter — direct-injection ready
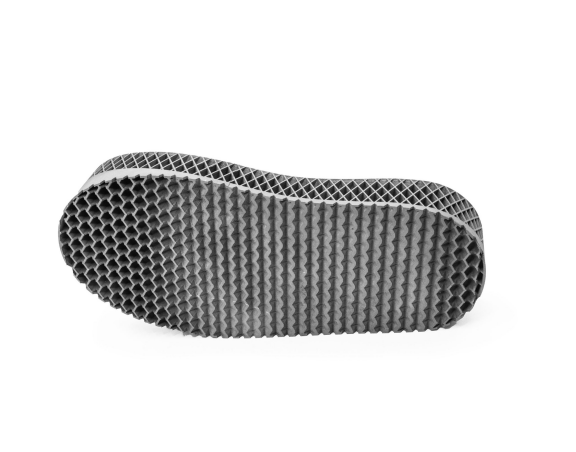
Figure 9: SLM-printed 316L midsole mold — angled view showing the diamond cross-hatch traction pattern and the integrated tread perimeter
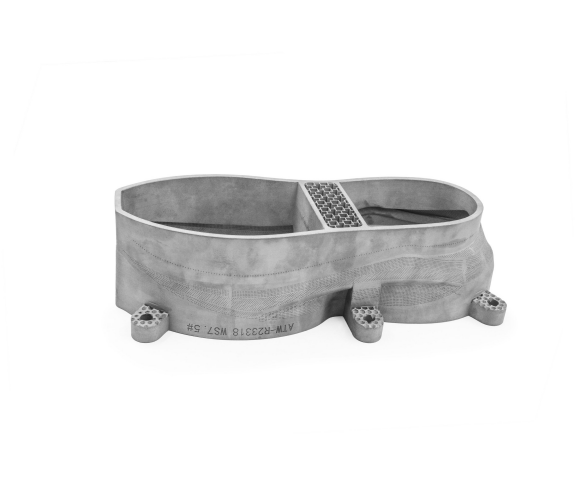
Figure 10: SLM-printed 316L stainless steel shoe-last (upper) mold — patient-specific geometry per size, mesh perforation pattern, part number 3D-marked in the build
4. The Result
· 50% cycle-time reduction — midsole cooling time 120 s → 60 s via AlSi10Mg conformal cooling
· 4 mold types, 3 alloys — AlSi10Mg, MS1, 316L — each matched to its specific duty
· 2-4 week lead time — vs. 12-16 weeks for CNC aluminum, first-article trials in 30 days
· 1000+ precision perforations — 316L outsole mold, corrosion-resistant for foaming service
· HRC 50–55 maraging mold — MS1 outsole mold, mirror-polished for direct EVA / TPU injection
· Monolithic construction — no welded inserts, no brazed cooling lines, no assembly drift
· Patient-specific lasts — 316L last mold, one geometry per shoe size, mesh perforation for upper forming
· 80% lead-time reduction — 4-week average across all four mold types, vs. 16-week CNC baseline
“We launched the new midsole lattice and the new outsole tread in 30 days, not 4 months. Aluminum for fast cycle, MS1 for wear, stainless for foaming service — three alloys, one supply chain, one CAD workflow.”
Materials: AlSi10Mg Aluminum | MS1 (1.2709) Maraging Steel | 316L Stainless Steel | Process: SLM Metal 3D Printing | Application: Multi-Material Footwear Molds