

MS1 (1.2709) Maraging Steel Conformal Cooling Mold Insert | SLM 3D-Printed Plastic Injection Mold Case Study
MS1 (1.2709) maraging steel plastic injection mold insert with internal conformal cooling channels, produced by SLM metal 3D printing. 16+ internal cooling ports, ±0.05 mm positional accuracy, HRC 50–55 after aging, 35% cycle-time reduction, 50% scrap reduction. Replaces drilled-insert cooling for high-cavitation molds.
Case Study: MS1 Maraging Steel Mold Insert with Conformal Cooling
Material: MS1 / 1.2709 (X3NiCoMoTi18-9-5) | Process: SLM + Aging | High-Cavitation Plastic Injection Mold
Metal 3D Printing Case Study
1. Background
A precision plastic injection molder was producing a 16-cavity thin-wall packaging part on a high-tonnage press. The legacy mold used a P20 tool-steel core with straight drilled cooling lines, and the cavity layout made it impossible to drill water lines near the gates. Result: the part warped at the corners, scrap rate ran 8%, and cooling time dominated the cycle. A conformal cooling insert in maraging steel — channels that follow the cavity geometry into the corners conventional drills cannot reach — was needed to bring cycle time and scrap rate under control.
2. The Challenge
Design requirements included:
· 16+ internal conformal cooling ports arrayed around the cavity layout, with channels that follow the cavity contour into the gate corners
· MS1 (1.2709) maraging steel — HRC 50–55 after aging, polishable to SPI-A3 mirror finish
· ±0.05 mm positional accuracy on every internal port relative to the cavity surface
· Channels with no support marks on the wetted surface (self-supporting geometry during printing)
· Through-hardening capability — uniform hardness from cavity surface to insert core, no soft spots
· Deliverable in 3 weeks for first-article trials
3. The Solution
The mold insert was redesigned with topology-optimized conformal cooling channels that wrap around the cavity layout — including the gate corners that the legacy drilled lines could not reach — and manufactured by Selective Laser Melting (SLM) in MS1 (1.2709) maraging steel powder. The SLM process printed the complex channel network, the central main inlet, the 16+ outlet ports, and the cavity-facing geometry in a single build with no brazed joints and no drilled lines. All channels were oriented to be self-supporting during printing, so the wetted surface is as-built — no support marks to break through or to seal.
After printing, the insert was stress-relieved at 490 °C, solution-treated at 820 °C, aged at 480 °C for 5 hours to reach HRC 50–55, then finish-machined on the cavity face and polished to SPI-A3. The maraging steel was chosen specifically because it hardens uniformly from surface to core (no decarburization risk), maintains dimensional stability through aging (<0.05% distortion), and polishes to the optical finish required for cosmetic packaging parts.
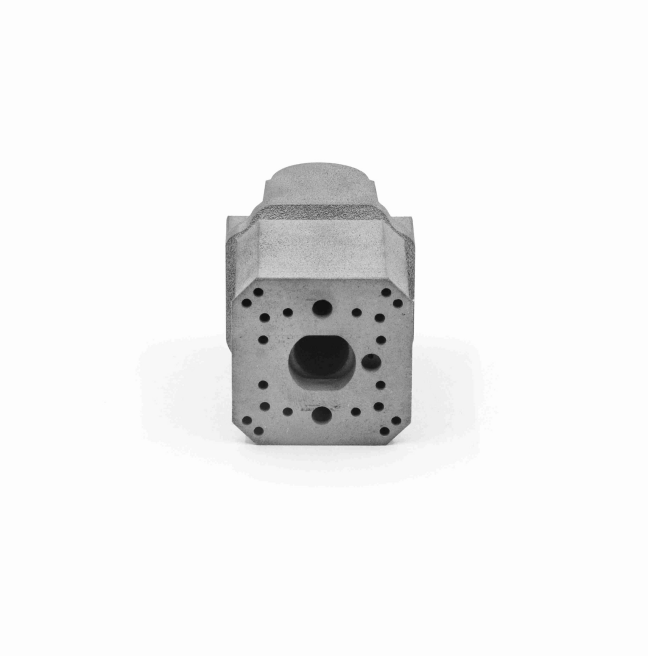
Figure 1: SLM-printed MS1 (1.2709) maraging steel mold insert — central main inlet, 16+ arrayed outlet ports, as-built wetted surfaces. After aging the insert reached HRC 50–55 and was polished to SPI-A3 on the cavity face.
4. The Result
· 35% cycle-time reduction — from 28 s to 18 s on the first optimized run
· 50% scrap reduction — from 8% to 4% — corner warpage eliminated
· HRC 50–55 uniform hardness — no soft spots, polish to SPI-A3 on cavity face
· ±0.05 mm port accuracy — 16+ channels, every port within tolerance relative to cavity
· Self-supporting channels — as-built wetted surface, no support marks to seal
· Lead time: 3 weeks — from CAD to aged, polished, ready-to-fit insert
“The conformal channels reached corners we could never drill to. Cycle time dropped by 35% on the first article, and the maraging steel polished to a mirror finish with no soft spots.”
Material: MS1 / 1.2709 Maraging Steel | Process: SLM + Aging | Application: Conformal Cooling Mold Insert